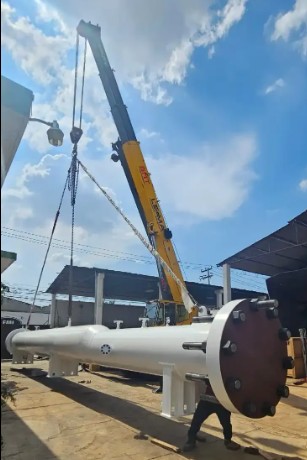
A coordination problem in five phases — engineering to commissioning.
01 · Objective
Deliver an ASME-stamped pig launcher trap — from design to on-site commissioning.
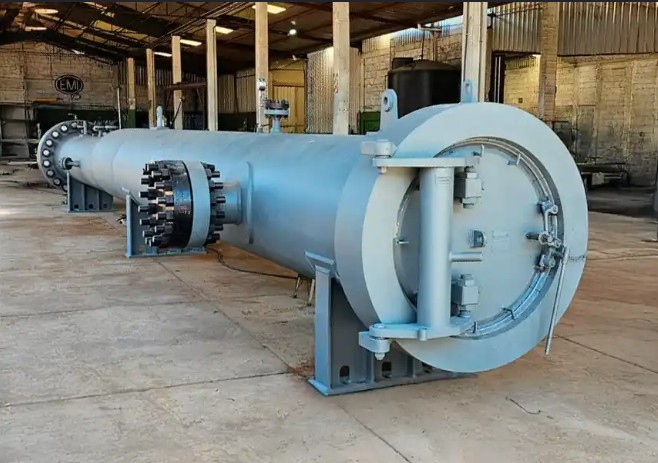
Full-cycle Project Management on a pig launcher pressure vessel: engineering, procurement, fabrication, testing, certification, delivery and commissioning — every phase traceable to ASME Section VIII and client specifications.
ASME Section VIII calculations — wall and nozzle thickness, materials, welding, internal pressure, connections.
Approval
Drawings and calculation memoranda submitted, reviewed and signed off with the client.
PM role
Controlled the engineering schedule and drove the design-approval loop to protect downstream dates.
03 · Phase 2 — Procurement
Buy the right materials, on the right dates, with the right certificates.
Scope of work
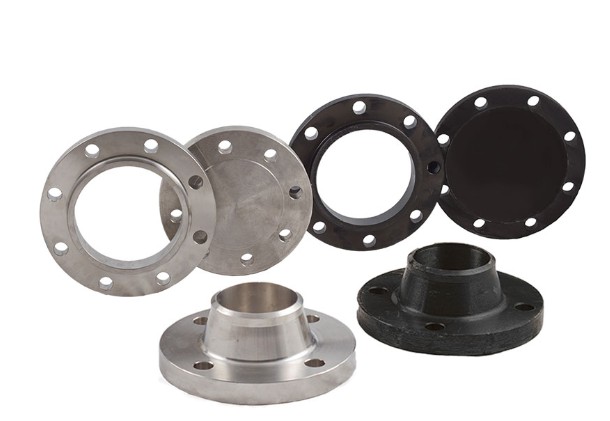
ASTM/API pipingFlanges + MTRsWelding consumablesCoating system
PM role
Supplier evaluationPO managementDelivery vs scheduleTraceability (MTRs)
04 · Team & my role
One PM. Five disciplines. One stamped vessel.
Coordinated engineering, procurement, production, QA/QC and HSE across the five phases, holding the schedule, cost and quality baseline from PO to sign-off.
05 · Phase 3 — Fabrication & inspection
Build to the drawing. Prove it with NDT.
01
Dimensional control of plate and pipe against approved drawings.
02
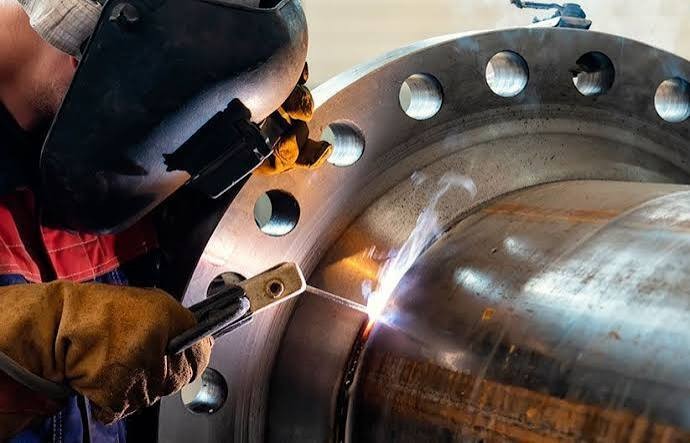
Qualified welding procedures (WPS/PQR) executed with certified welders.
03
Pre-assembly release before final joining — every sub-assembly checked and signed off.
04
Non-destructive testing — VT, PT and RT — coordinated with the inspection body.
05
PM: construction schedule control, area coordination and weekly progress reports to the client.
06 · Phase 4 — Testing, painting & certification
No paint until the vessel proves itself.
Hydrotest
Pressure test at 1.5× design pressure, witnessed and signed by the ASME inspector before any surface work.
Coating
Surface preparation and painting released only after hydrotest approval — sequencing protected the schedule and the finish.
Dossier
QA/QC pack closed out: calculation memos, ITPs, as-builts, NDT and welding procedures, release protocols and final tests.
PM role
Coordinated the hydrotest with the ASME inspector, monitored execution and issued the approval to paint.
07 · Phase 5 — Delivery & commissioning
A stamped, tested vessel — installed, connected and signed off.
Transport
Coordinated rigging, transport and site installation with the client's logistics team.
Hook-up
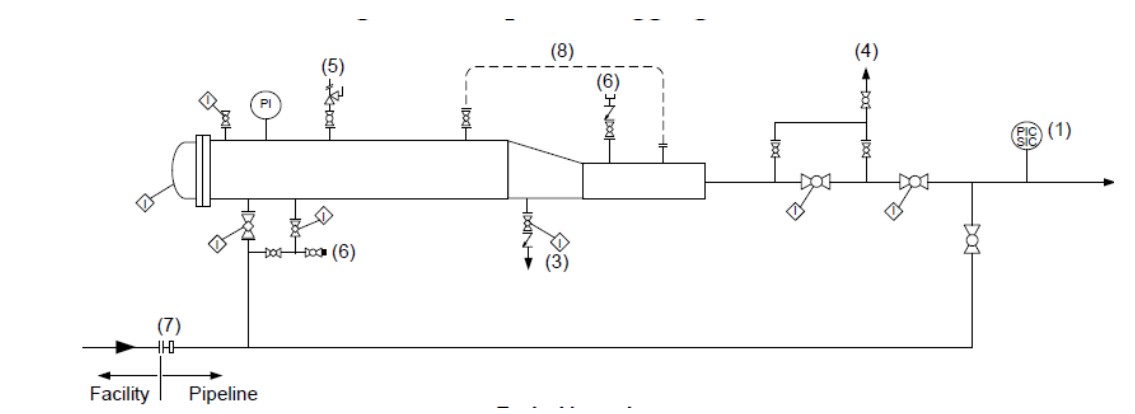
Connection to process lines and instrumentation validated against the P&IDs.
Tightness
On-site tightness tests witnessed with the client before start-up.
PM role
Transport coordination, on-time delivery and client sign-off — the trigger for invoicing.
ASME
Section VIII stamp
0
Phases delivered end-to-end
1.5×
Hydrotest vs design pressure
A pressure vessel delivered on schedule, on budget and to ASME code — coordinated across engineering, procurement, fabrication, certification and commissioning by a single project owner.